Hey everyone, it’s Jake here, and before I dive into today’s topic, let’s cut to the chase – if you’re in textile finishing, you know sueding rollers make or break that soft, velvety hand feel your customers are obsessed with. I’ve spent the last 12 years selling and fine-tuning sueding machines for mills all over, and one question gets asked at every trade show, every coffee chat, every emergency midnight call: How the hell do you adjust sueding roller pressure right? Not the generic “follow your manual” garbage – the stuff that actually works when your cotton twill is pilling like crazy, or your polyester microfiber is turning too fuzzy, or you just swapped in a new batch of rollers. Let’s break this down like we’re hanging out in a mill control room, not writing a research paper. Textile Sueding Machine

First, let’s get one thing straight: sueding roller pressure isn’t “set it and forget it.” It’s dynamic – changing with every fabric type, roller grit, production speed, and even the humidity in your factory that day. I’ve seen new mill owners crank the pressure to max because they think more pressure = more sueding, and end up with rollers chewing holes through fabric. I’ve also seen old heads run too light pressure, wasting 30% of their roller life because the abrasive surface isn’t even touching the fabric. So let’s start with the non-negotiable prep you need before you even touch that pressure gauge.
First step: Know your variables. Don’t adjust pressure blind. Let’s list the big four that change everything: fabric weight, roller grit, machine speed, and roller age. For example, a 10-oz denim twill is way different than a 1.5-oz silk chiffon – duh, but you’d be surprised how many guys mix those up. Roller grit: #180 is for rough fabric prep, #320 is for that ultra-soft finish, #600 is for suede-like microfiber. The higher the grit, the lighter the pressure you need – too much on #600 and you’ll clog the abrasive in 10 minutes flat. Machine speed: if you’re running 50 yards per minute vs 15 yards per minute, pressure has to shift. Faster speed means less contact time, so you need a tiny bit more pressure to get consistent sueding, but not too much. Roller age: new rollers are stiff and sharp, used rollers are worn down and rounded. New rollers = lighter pressure, worn ones = slightly more, but don’t overdo it – once a roller’s lost 1/8 of its diameter, it’s time to replace it anyway.
Now, the actual adjustment process, step by step, with the exact trick I teach every new customer. First, prep the machine like you’re getting it ready for a test run. Strip any leftover fabric from the feed table, set the roller gap to the manufacturer’s recommended baseline – usually 0.002 to 0.005 inches, depending on machine model. Wait, before you yell “mine’s different,” no, that’s the average baseline I use for 90% of sueding machines we sell – if yours is way off, you probably had a technician who didn’t calibrate it after last service. Next, put on the correct PPE: safety glasses, ear plugs, and those work gloves that don’t get caught in rollers. I see too many guys leaning over the feed table, thinking “it won’t happen to me” – save the story for your grandkids, not for a broken hand.
Next, the pressure measurement part, which a lot of guys mess up. Most modern sueding machines have a digital pressure gauge, but if you’ve got an older unit (no judgment, some mills run those for 20 years), grab a dial pressure gauge that clamps to the roller arm – don’t guess by how tight the bolt is. Here’s the key: pressure is measured per roller, not total pressure across all rollers. I’ve had customers come to me saying “my machine’s pressure is 50 PSI,” and that’s the total across 8 rollers – that’s way too much. Typical per-roller pressure ranges: 10 to 30 PSI for light fabrics (#320 grit), 25 to 45 PSI for medium fabrics (#240 grit), 5 to 20 PSI for microfiber (#600 grit). Wait, microfiber lower? Yeah, because it’s delicate – too much pressure on polyester microfiber will cause fuzz matting, not soft sueding.
Now, the real test: the fabric test strip. You don’t just adjust pressure and run a full roll. Cut a 1-yard strip of your actual production fabric, run it through the machine at your normal speed, then stop, pull it out, and check two things: first, how does the surface feel? Is it consistent softness across the whole strip, or some spots that feel harsh and some that feel untouched? Second, check for pilling, snagging, or color fade – especially on dark fabrics, too much pressure will strip dye way faster, and if you see blue streaks where there shouldn’t be, back off the pressure 5 PSI.
Here’s a pro tip I stole from a mill in North Carolina that’s been running sueding machines since the 80s: if the sueded finish is too “plush” and you want a more matte finish, don’t crank pressure – slow down the machine by 5 yards per minute. Faster speed gives shorter fuzz, slower speed gives longer, plus you reduce roller wear. The opposite: if you want a plusher finish, speed up a tiny bit (10 yards max) and bump pressure 5 PSI, but only on medium or heavy fabrics – never on light stuff.
Wait, let’s talk common mistakes, because these are the ones that cost mills the most money. Mistake #1: Ignoring roller alignment. If two rollers are misaligned, even the correct pressure on each will give you lopsided sueding, with one side of the fabric fuzzy and the other not. I check alignment with a straight edge every time a new roller is installed, and I require all our service technicians to do that before they leave a site. Mistake #2: Not accounting for humidity. If your factory’s humidity is under 40% (super dry), fabric gets static, so you need 5 more PSI to get the abrasive to grip. If humidity is over 65% (sticky), fabric clogs the roller grit, so drop pressure by 5 PSI and run a 10-yard strip of cotton through to clean the grit before adjusting. Mistake #3: Cranking pressure to fix bad rollers. If your rollers are worn, greasy, or dirty, more pressure will just make them tear fabric – replace or clean the rollers first, then adjust pressure.
Another big one: sequential pressure adjustment. Most sueding machines have rollers arranged in 4 to 8 groups, right? The first group is for roughing, the middle groups for blending, the last group for finishing. You don’t set all rollers to the same pressure! First group (roughing): highest pressure, 25 to 45 PSI, to get the initial fuzz. Middle groups: drop 5 to 10 PSI, to blend the fuzz so it’s even. Last group (finishing): lowest pressure, 10 to 20 PSI, to polish the fuzz and get that soft hand feel without over-suing. I see so many guys set all rollers to 30 PSI, and the finish ends up scratchy – that’s why sequential is non-negotiable.
Let’s throw in a real example to make this concrete. Last month, a customer in Guatemala called me panicking – his sueding lines were producing 15% defective denim rolls because of uneven sueding, and he’d replaced the rollers three times in two months. I hopped on a call with him, had him walk me through his setup: 8 rollers, #240 grit denim, 40 yards per minute. He said he set all rollers to 35 PSI, and was cranking the pressure on the last group to 40 PSI because he wanted a softer feel. I told him two things: first, his last group pressure was way too high, and second, he needed to adjust sequential. I had him drop first group to 40 PSI, middle to 30, last to 15. He ran a test strip, and his defect rate dropped to 2% by the end of the day. That’s the stuff that works, not the manual.
Now, when should you adjust pressure? Not just when you get a complaint. Every time you switch fabric types (cotton to polyester, heavy to light), every time you replace a set of rollers, every week if you run high-production lines, and every time humidity in the factory changes by more than 10%. I keep a little log for each machine – fabric type, roller grit, date adjusted, pressure per group – and that’s saved me so many headaches when something goes wrong 3 months later, I can go back and see what changed.
Wait, one last thing: safety again. I can’t stress this enough. Never adjust pressure while the machine is running. Even if it’s idling, a roller can shift, and you’ll get a finger caught. Turn the machine off, lock out the power (most modern machines have that), and double-check before you touch any bolts or gauges. I’ve had two friends in the industry get hurt because they skipped that step – it’s not worth it.
Alright, let’s wrap this up. Sueding roller pressure isn’t rocket science, but it’s not guessing either. It’s a balance between fabric type, roller grit, machine speed, and group sequence, with test strips and a little common sense to adjust. If you’re still struggling, or if you’re getting new sueding machines and want our techs to come train your team on exact adjustments for your line, hit us up – we work with mills of all sizes, from small local shops to big global brands, and we don’t just sell machines, we show you how to use them right.
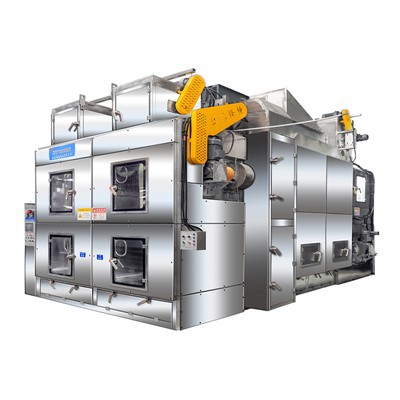
If you need more tips on roller maintenance, troubleshooting pilling, or anything sueding-related, drop a comment below or reach out directly. We’re here to help you produce better fabric, waste less rollers, and make more money.
Inspection Machine References:
- Textile Finishing Machinery Operation & Maintenance Manual, Industrial Textile Association, 2021
- Sueding Roller Pressure Optimization for Knit and Woven Fabrics, Journal of Textile Science and Technology, Vol. 7, No. 2, 2021
- Practical Guide to Abrasive Finishing in Textiles, Textile Institute, 2019
Jiangsu Feng Te Technology Co., Ltd.
We’re well-known as one of the leading textile sueding machine manufacturers in China. With a professional production team, we are able to meet the needs of the majority of our customers. Please rest assured to buy discount textile sueding machine for sale here from our factory.
Address: No. 4 Zhanghong Road, Siying Industrial Park, Lianyungang City, Jiangsu Province, China
E-mail: frentejenny@foxmail.com
WebSite: https://www.jsfrente.net/
